WhatsApp
 jessica.chai@ltzzc.com
 0086-379-69950051

How Heavy Duty Slewing Bearing Resists Moment Loads
How can engineers determine whether a slewing bearing will resist the overturning moment created by an offset load, long boom, raised platform, or rotating attachment? The answer is not found by checking axial load alone. A Heavy Duty Slewing Bearing must be assessed as a combined-load component that carries axial force, radial force, and overturning moment at the same time.
Moment load is often the governing condition in rotating equipment. A suspended payload may be moderate in weight, yet its distance from the bearing center can create a large overturning effect. The bearing then sees higher localized contact stress in one section of its raceway while another section may unload. If that condition is ignored during early design or retrofit planning, the result can be uneven rotation, mounting distortion, abnormal gear engagement, shortened raceway life, or damage to the surrounding structure.
This article explains how moment resistance works in practice, which design inputs affect it, and where the physical limits sit. For an initial product comparison, review LTZC’s precision slewing bearing range alongside the working loads and installation layout of your machine.
Start with the actual combined load condition
Conclusion: Select a bearing from the complete duty cycle, not from the largest vertical load by itself. Moment capacity depends on how axial load, radial load, and overturning moment occur together, because these forces change the internal load distribution around the raceway.
The usual source of moment load is an offset force. A load applied directly above the bearing center creates mainly axial force. Move that same force outward, and it creates a turning effect around the bearing center. The basic relationship is simple: overturning moment equals applied force multiplied by the distance from the bearing center. A longer arm therefore raises moment demand even when the payload does not change.
In real machines, the applied force may come from more than the payload. Engineers should include attachment weight, boom weight, tool reaction, wind exposure where relevant, acceleration and braking forces, cable forces, hydraulic cylinder reactions, and any shock condition expected during operation. The maximum load case may occur at a position that is not visually obvious. For example, a boom can produce a more severe bearing moment during starting, stopping, or side loading than during a static lifting position.
| Load input | What it affects in practice | What can go wrong if omitted |
|---|---|---|
| Axial force | Loads the bearing in the direction normal to its mounting faces. | Raceway contact stress may be underestimated during lifting or pressing duties. |
| Radial force | Acts across the bearing center and can influence rolling element loading and gear alignment. | Rotation can become rough or gear mesh can become inconsistent under side force. |
| Overturning moment | Concentrates load into part of the raceway and loads the mounting structure unevenly. | A bearing selected only for vertical load may lose usable life or mounting stability. |
| Dynamic force | Adds transient load from acceleration, braking, impact, or changing machine posture. | A static calculation may not represent the most severe operating condition. |
| Mounting deformation | Changes how force transfers from the machine structure into the bearing rings. | Even a correctly sized bearing can receive uneven internal loading. |
This approach fits cranes, welding positioners, excavating attachments, aerial platforms, radar equipment, marine deck machinery, and large rotating fixtures. It does not replace a machine-level structural review. If the support frame deflects, bearing catalog data alone cannot predict the final internal load pattern.
Build the load case before requesting a bearing proposal
Provide the bearing supplier with a drawing or clear description of the support structure, the load application point, rotation axis, required rotation range, drive arrangement, and operating positions. Also identify whether loads are continuous, intermittent, reversing, or shock-prone. These details allow the supplier to evaluate a realistic combined load rating instead of treating the bearing as an isolated part.
Identify all forces acting on the rotating structure.
Measure each force location relative to the bearing center.
List operating positions that change load direction or lever arm.
Separate normal operating loads from infrequent peak events.
Describe acceleration, braking, impact, and vibration conditions.
Provide mounting ring and support-frame information.
LTZC provides customized bearing solutions based on working conditions, existing designs, and technical specifications. This is useful when a retrofit has fixed bolt locations, a constrained envelope, or an existing drive arrangement that cannot be substantially changed.
Understand the boundary set by raceway geometry and bearing diameter
Conclusion: Raceway geometry and bearing diameter establish a physical boundary for overturning-moment capacity. A larger bearing diameter can increase the lever arm through which internal forces resist moment, while raceway geometry determines how effectively rolling elements receive and distribute those forces. Neither factor can be evaluated alone.
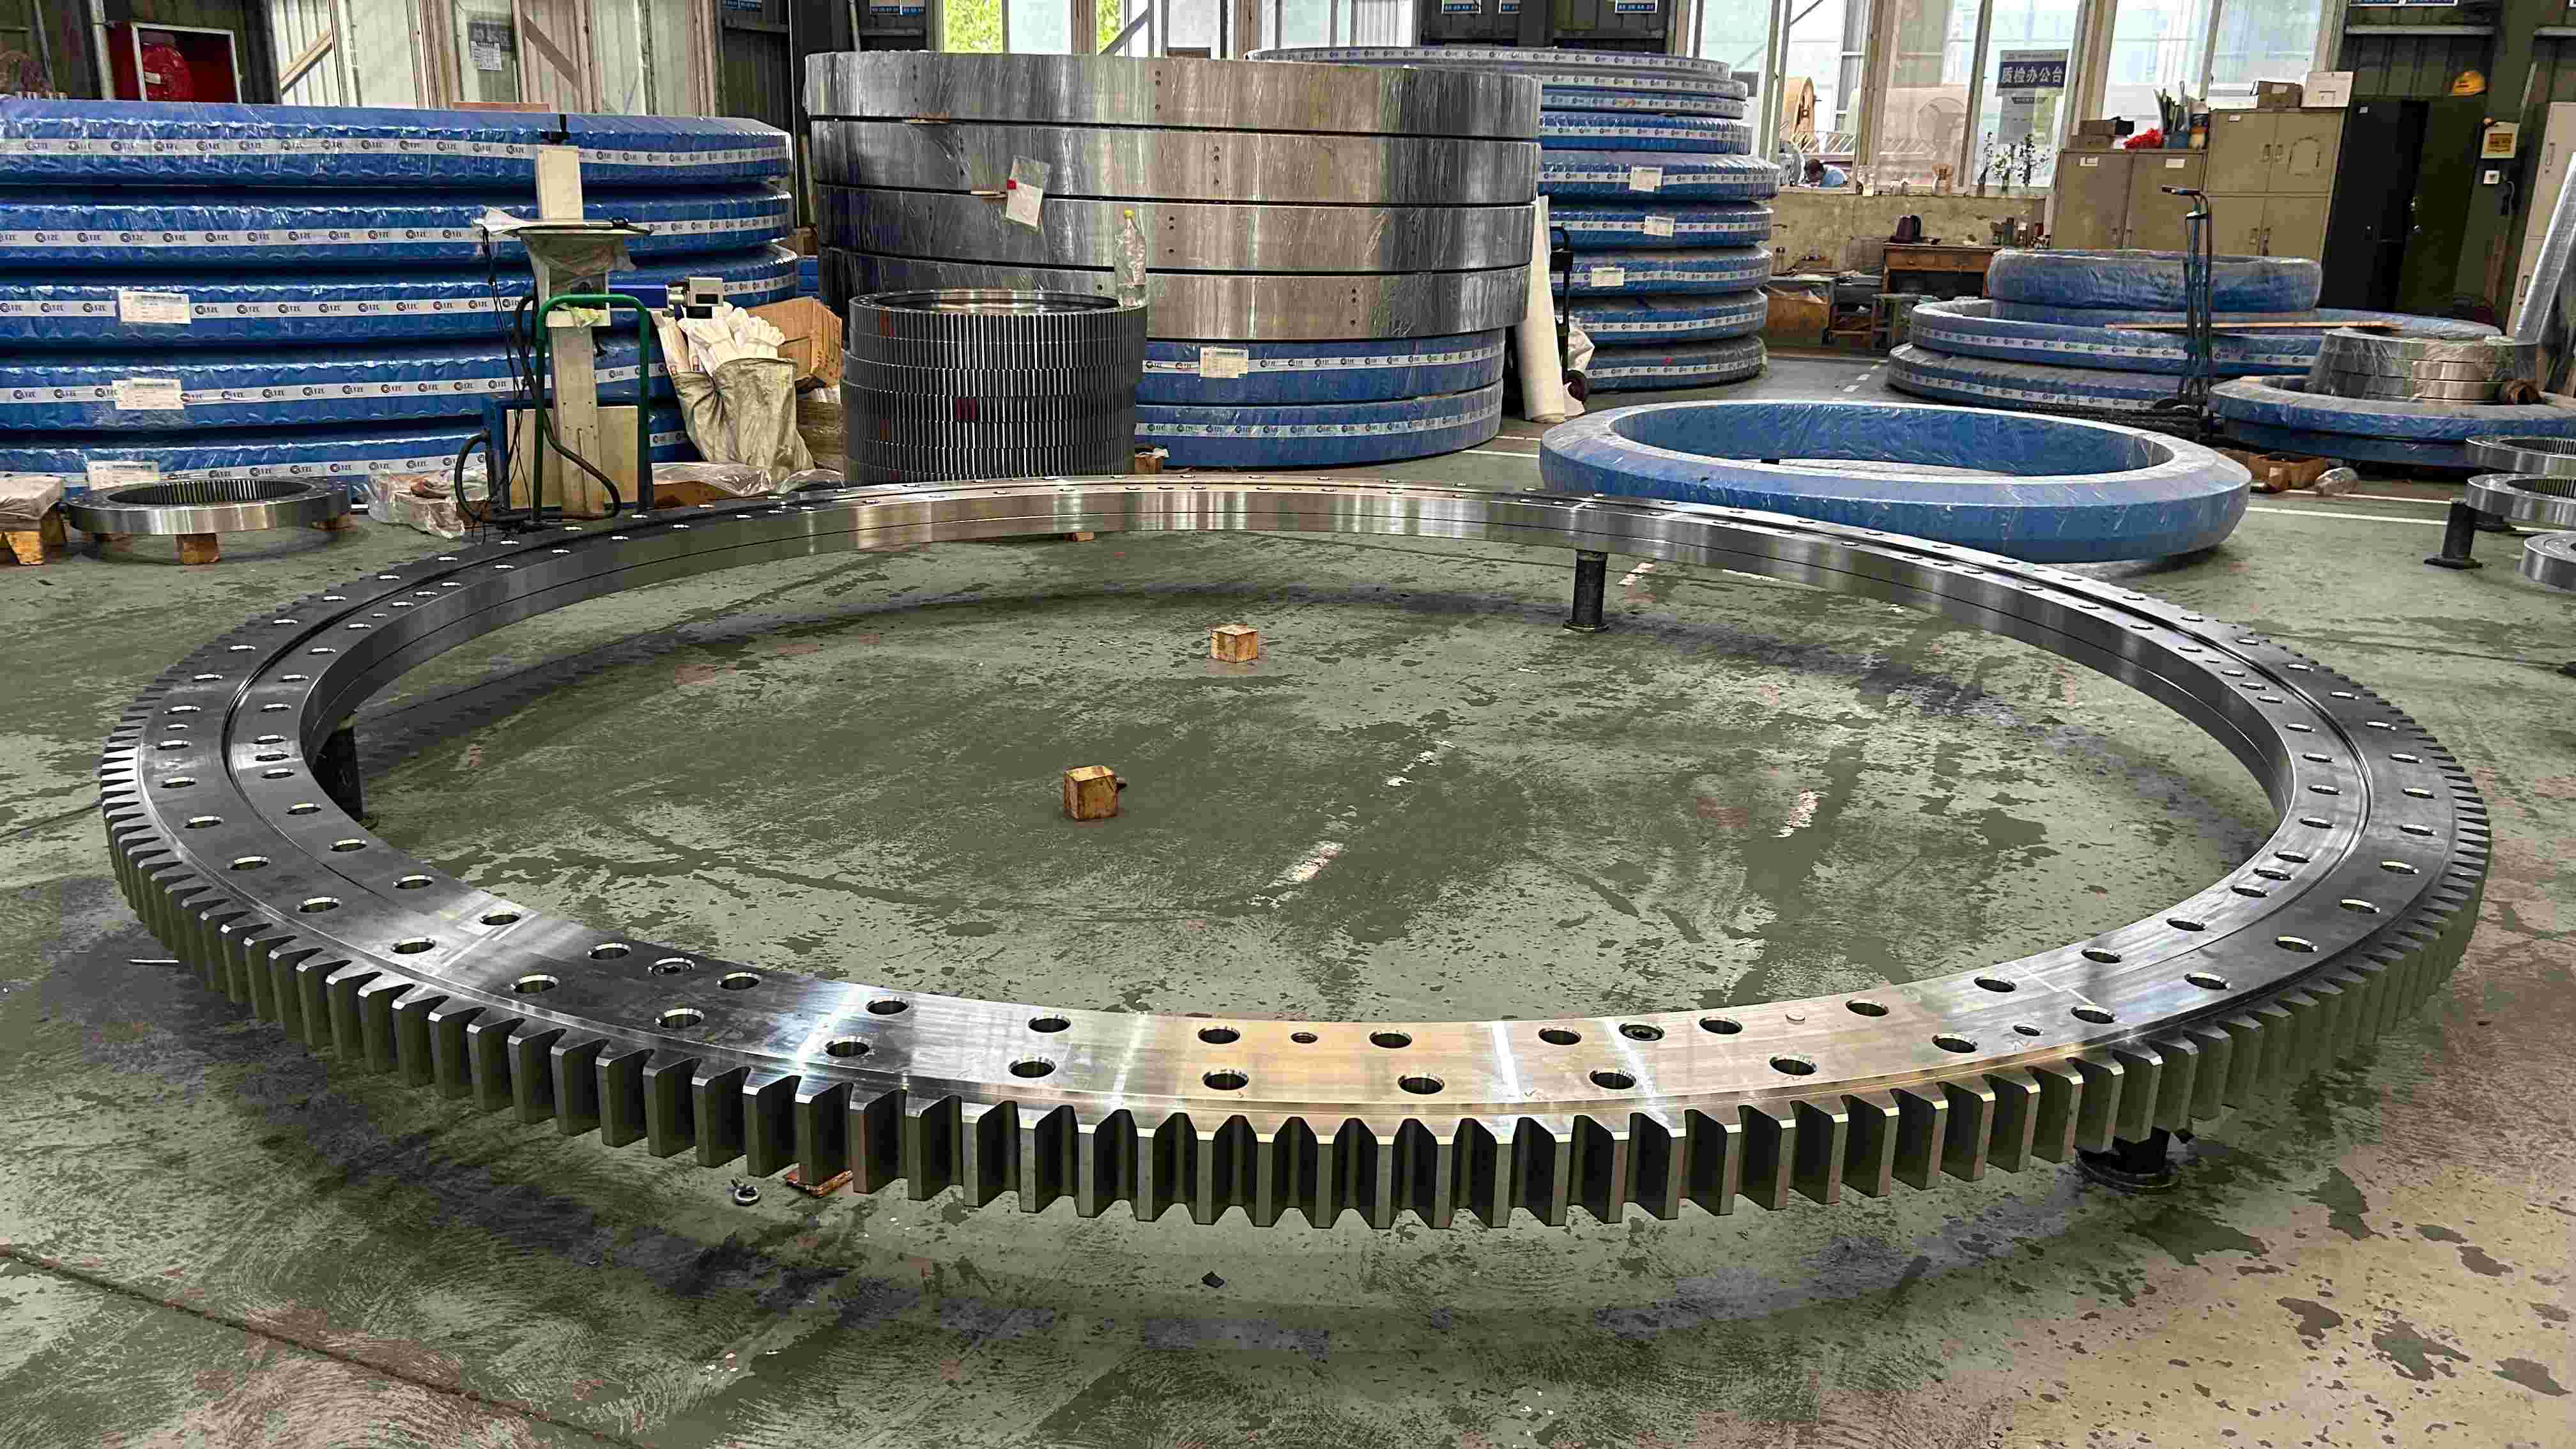
When an overturning moment acts on a slewing bearing, one area of the bearing carries increased load while the opposite area becomes less loaded. The bearing resists this tendency through internal contact forces transmitted between rolling elements and raceways. The distance between heavily loaded and lightly loaded regions matters. A larger bearing diameter generally provides a wider force path, which can improve resistance to moment load when the rest of the bearing design and mounting structure are suitable.
However, a larger diameter is not an automatic answer. The chosen ring section, raceway profile, rolling element arrangement, ring stiffness, mounting bolt pattern, and support flatness also determine whether that diameter can be used effectively. A large but lightly supported ring can deform under load. In that case, theoretical diameter advantage is reduced because contact becomes uneven.
| Key parameter | What it actually changes | Buyer risk when selected incorrectly | Best use case |
|---|---|---|---|
| Raceway geometry | Controls rolling element contact position, contact distribution, and the bearing response to axial, radial, and moment loading. | Localized stress can rise if the raceway arrangement does not suit the direction and combination of loads. | Applications with changing load direction, offset payloads, or repeated rotation. |
| Bearing diameter | Changes the force lever arm available to oppose an overturning moment. | A small diameter may concentrate internal forces when a long boom or wide attachment creates high moment. | Large rotating structures where installation space permits an appropriate diameter. |
| Ring section stiffness | Helps the rings maintain raceway alignment under concentrated loading. | Ring distortion can create uneven contact and rough rotation. | Machines with high local mounting loads or nonuniform support. |
| Rolling element arrangement | Influences how loads are shared internally and what directions can be carried effectively. | The bearing may be poorly matched to radial force, axial force, or moment direction. | Equipment with known combined-load conditions. |
| Mounting support stiffness | Determines whether the bearing receives the load pattern assumed during selection. | Frame deflection can negate the benefit of a suitable raceway and diameter. | Retrofits, fabricated structures, and large welded assemblies. |
Raceway geometry is particularly relevant when an application alternates between different load directions. A bearing that performs well under predominantly axial loading may not be the right arrangement for a machine that also sees persistent radial force and high overturning moment. The correct choice depends on the real duty, not on a single headline capacity value.
This boundary also applies to compact equipment. If the machine envelope fixes the maximum bearing diameter, the design team may need to reduce the offset load, strengthen the support structure, revise attachment geometry, or reconsider operating limits. Simply specifying a heavier bearing within the same restricted diameter may not solve the moment problem. That is the limit of a component-only fix.
Match the bearing arrangement to load direction and rotation duty
Conclusion: Choose the bearing arrangement after identifying the dominant load direction and duty pattern. The best option for a slowly indexing fixture is not necessarily the best option for continuously rotating machinery with changing radial load.
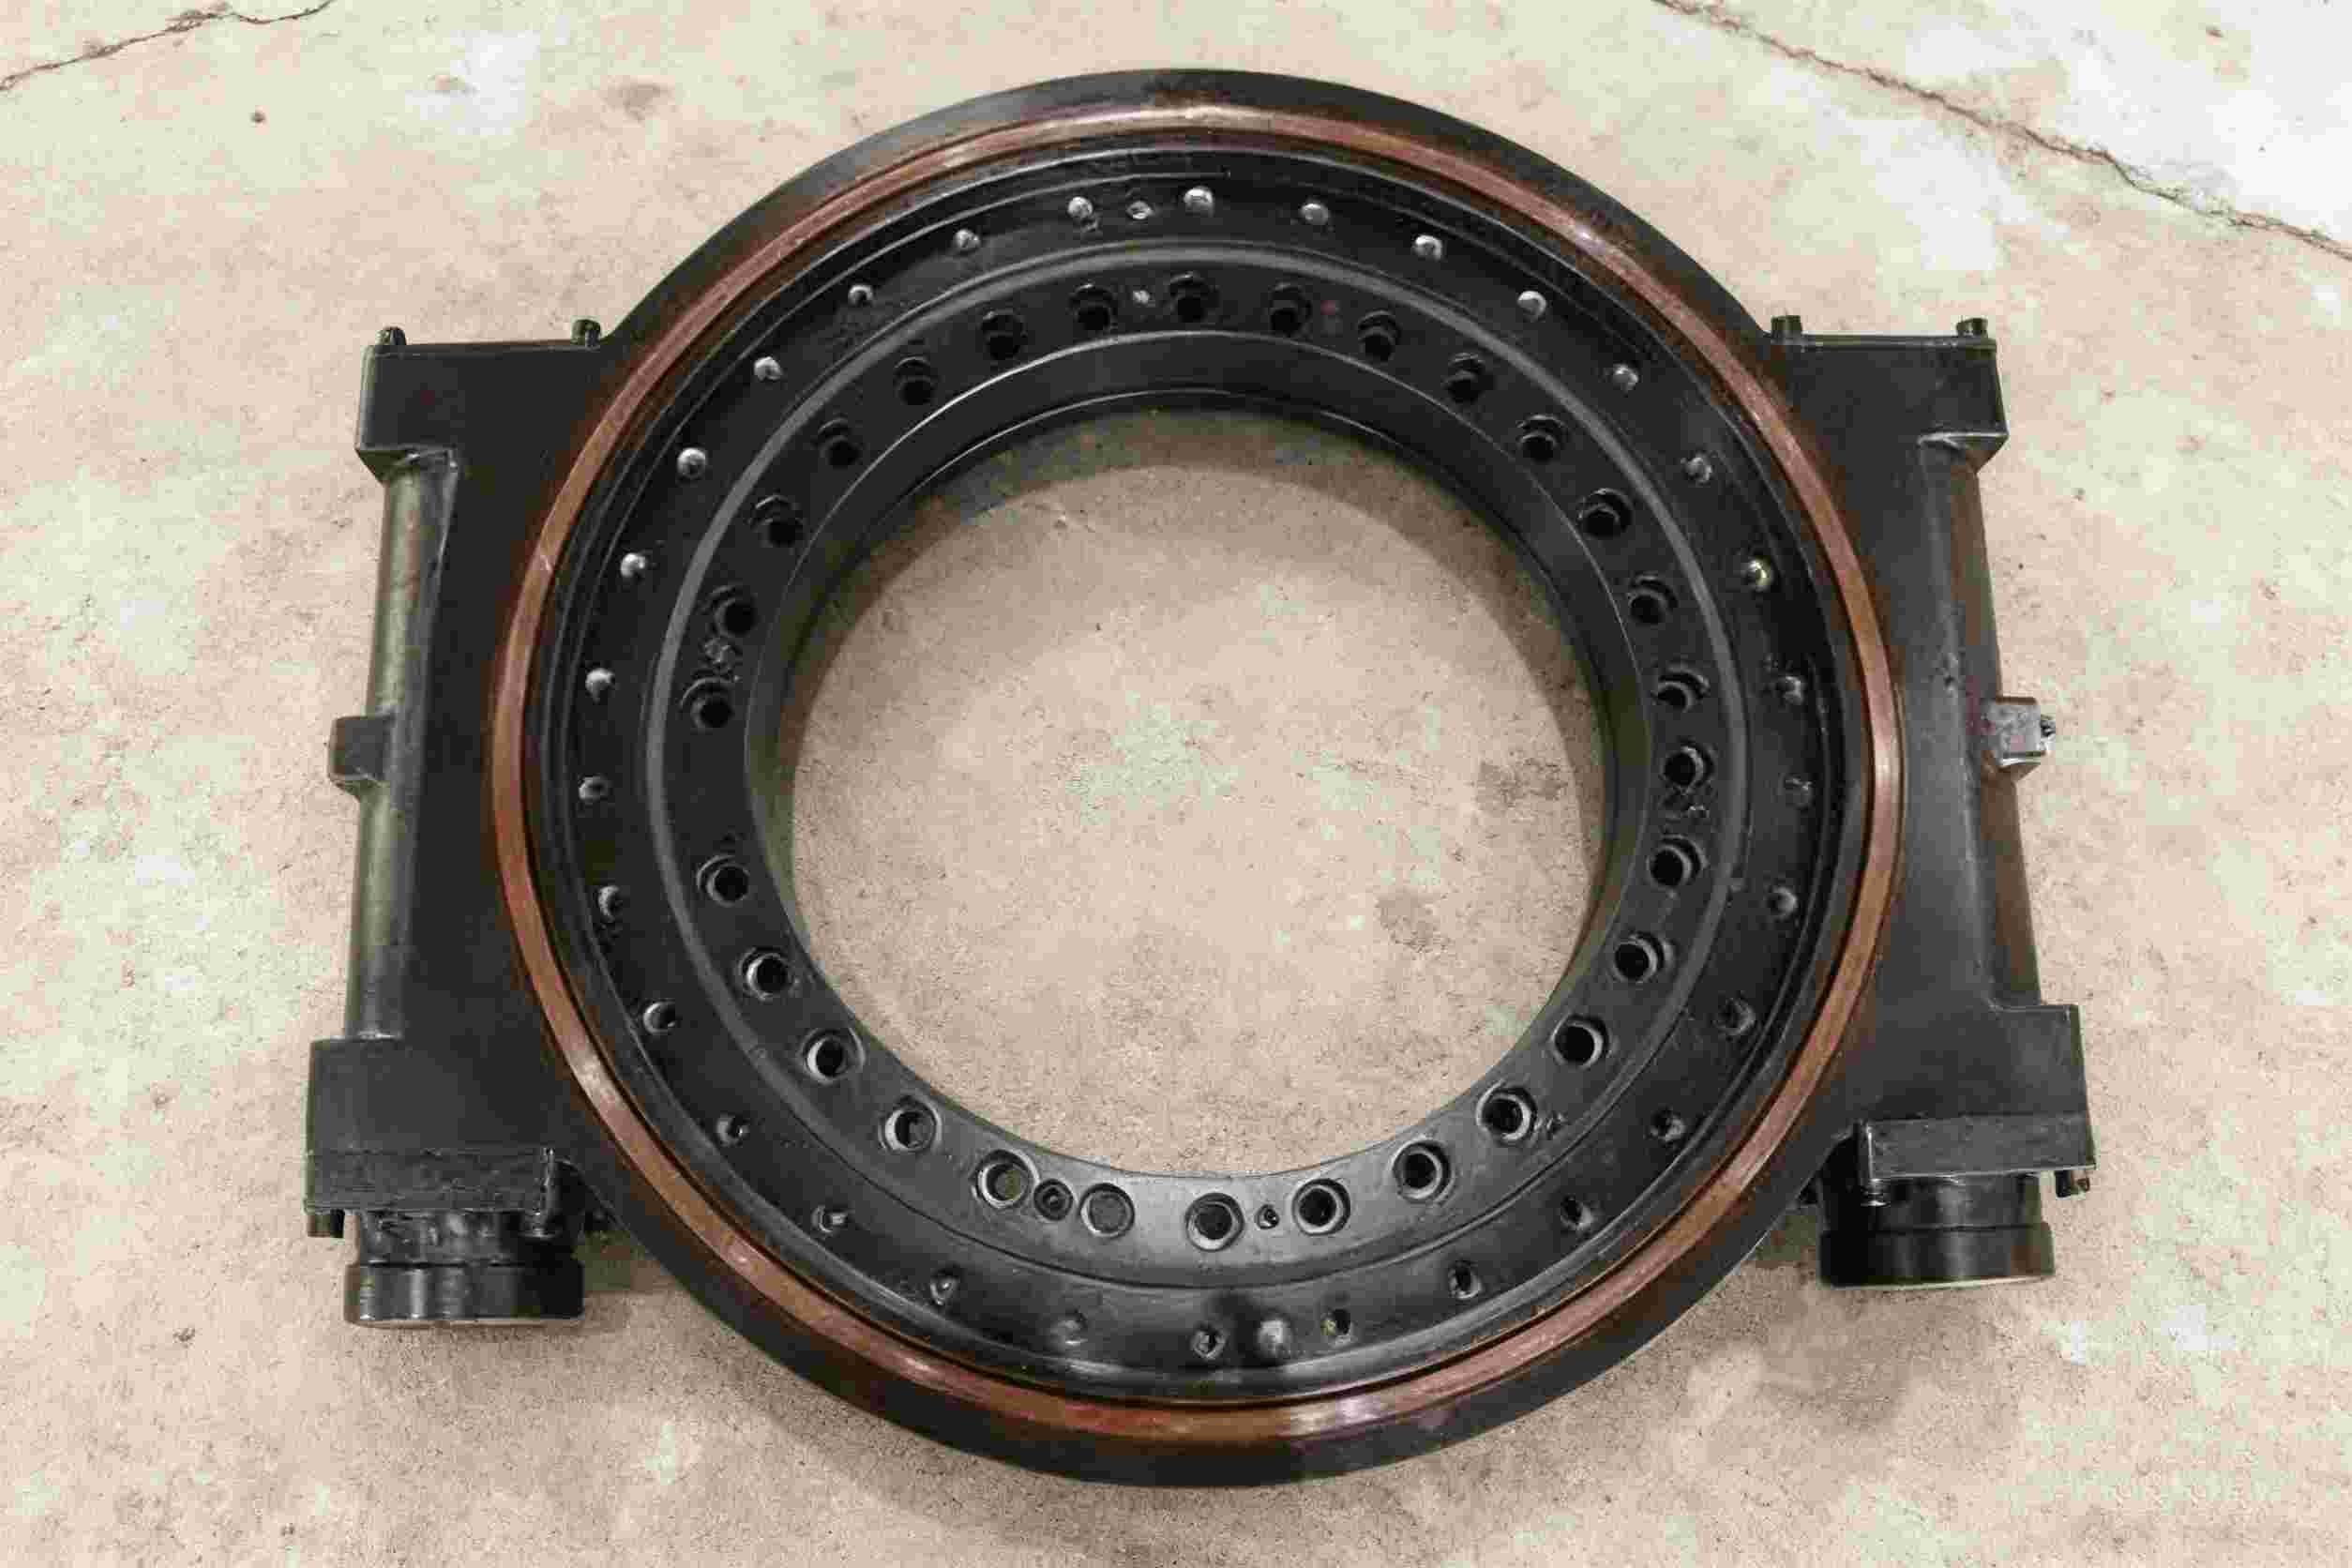
Single-row and multi-row bearing arrangements, as well as ball and roller designs, can respond differently to combined loading. The selection should account for load direction, required stiffness, friction behavior, available installation space, gear integration, and rotation pattern. A supplier should verify the intended arrangement against the combined load case rather than relying on a nominal size comparison.
| Selection question | Why it matters | When the answer changes the bearing choice |
|---|---|---|
| Is rotation continuous or intermittent? | Duty pattern affects lubrication planning, heat generation, and wear exposure. | Continuous rotation generally needs closer attention to lubrication and drive interaction. |
| Does radial load act in one direction or reverse? | Changing radial force alters which raceway area carries the load. | Mobile equipment and rotating attachments may see direction changes through the operating cycle. |
| Is high stiffness required at the tool point? | Bearing deflection and support deflection can affect process accuracy. | Machining fixtures, welding equipment, and measuring systems may prioritize stiffness. |
| Is an integral gear required? | Gear form, drive position, and backlash needs must work with bearing loading. | Compact rotating systems often combine bearing and drive functions. |
| Is the project a retrofit? | Existing bolt holes, central opening, and drive location can limit options. | Replacement work may require a custom interface rather than a standard ring. |
Where the bearing includes gear teeth, moment loading can also affect drive behavior through ring deflection and mounting movement. Review the mating pinion and consider the complete slewing ring gear interface rather than treating the gear as separate from the bearing. This is especially relevant when the drive is mounted on a flexible bracket or when the rotating frame has uneven support.
If a compact rotary unit is preferred, compare the bearing and transmission layout with available Slewing Drives. A self-contained drive option may suit some applications, but it does not remove the need to verify moment load at the mounting interface.
Protect moment capacity through mounting design and installation control
Conclusion: A bearing can only resist the moment load it was selected for when both mounting faces support the rings evenly. Flat, stiff, and properly prepared interfaces allow the load to transfer around the ring as intended.
Mounting errors are a frequent reason for poor field performance. A ring installed on a distorted support can be forced out of shape before it carries any operating load. Under moment, the existing distortion combines with external loading and creates high contact concentration. Loose fasteners, uneven tightening, paint buildup, weld spatter, burrs, and unsupported sections of a mounting flange can all contribute to this problem.
Use clean mating faces: Remove burrs, debris, weld residue, and localized high spots so the ring seats consistently.
Check support continuity: The ring should not bridge gaps or rest on isolated high areas, because this promotes distortion under load.
Follow the specified tightening sequence: A controlled pattern helps avoid pulling one part of the ring down before the rest is supported.
Review bolt retention: Moment load repeatedly changes the load distribution through the mounting joint, so fastener condition must be monitored.
Verify drive alignment: Gear mesh should be assessed after installation because support deformation can alter engagement.
Plan lubrication access: Inaccessible lubrication points invite neglected maintenance and higher internal wear.
These actions suit both new equipment and replacement projects. They do not correct a support frame that is fundamentally too flexible. If the structure moves excessively under service load, redesign of the surrounding frame or flange may be necessary before changing the bearing.
For practical preparation and service checks, see LTZC’s bearing installation guidance. Installation information should be used with the bearing-specific drawings and technical instructions supplied for the selected unit.
Use a structured selection review before approving a design
Conclusion: A selection review should end with a documented load case, interface review, and supplier confirmation. This prevents the common mistake of approving a bearing based on outside diameter or static vertical load alone.
For early planning, engineers can use the following checklist before releasing an RFQ or finalizing a retrofit drawing.
Define the rotation center: Establish the bearing centerline and identify every force location relative to it.
Calculate overturning moment: Include offset payload, attachment self-weight, actuator reaction, and dynamic force sources where relevant.
List combined load cases: Record axial, radial, and moment loads occurring together in each machine position.
Review the support structure: Identify flange thickness, frame stiffness, mounting bolt layout, and any areas without continuous support.
Confirm functional constraints: Include central opening, gear requirement, rotation range, environment, lubrication access, and replacement interchange needs.
Submit drawings and duty information: Ask for selection feedback based on the complete operating condition.
Plan verification after installation: Check seating, bolt condition, rotation smoothness, and gear engagement before full service.
A common error is assuming that a bearing with a larger outside diameter will always provide adequate overturning moment capacity. Diameter matters, but it must work with suitable raceway geometry, ring stiffness, mounting support, and the actual combined loads. Another error is using a prior machine design as proof of suitability. A new attachment, longer arm, higher payload position, altered drive, or more frequent duty can change the loading enough to require a fresh review.
LTZC Bearings Co.,Ltd. operates under ISO9001:2015, ISO14001:2015, and ISO45001:2018 management system certifications and is certified by ISO, CCS, and ABS. For projects with fixed production schedules, stated delivery is 30–90 days, and no MOQ is required. These points can be useful for prototype work, replacement planning, and custom bearing requests where a standard catalogue item does not match the interface or working condition.
Jessica.chai, Slewing Bearing Engineer, supports global industrial clients with selection and after-sales service for slewing bearings, slew drives, and thin-section bearings. Submit your load table and mounting drawing to request selection advice for your application.
===